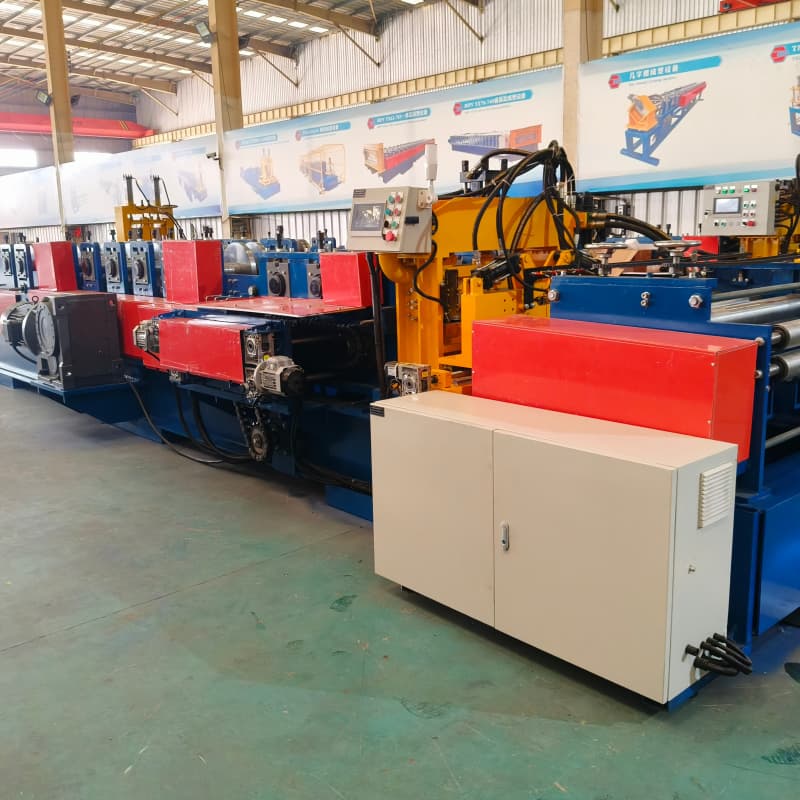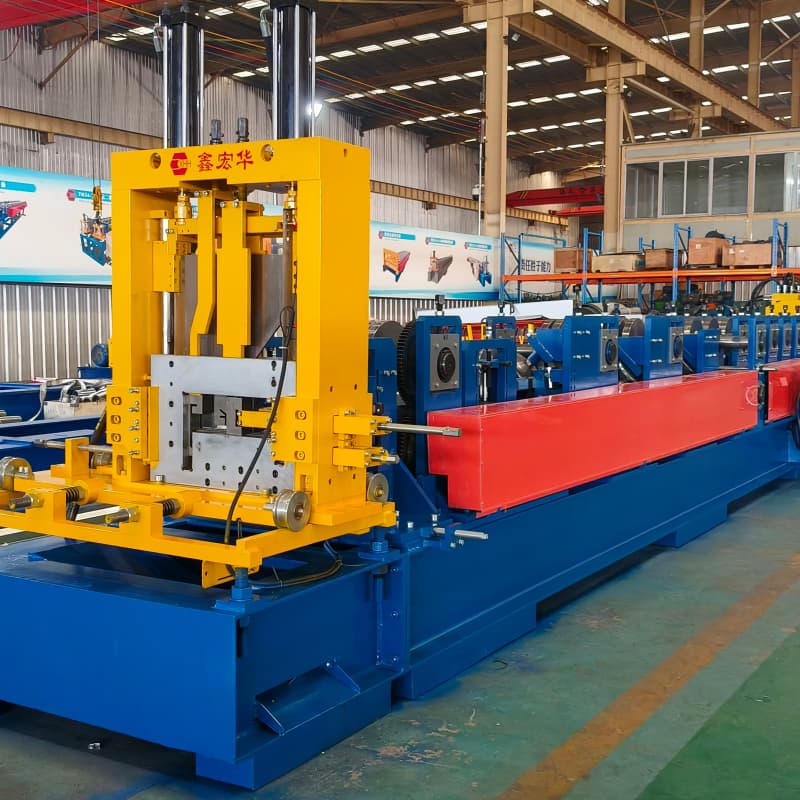
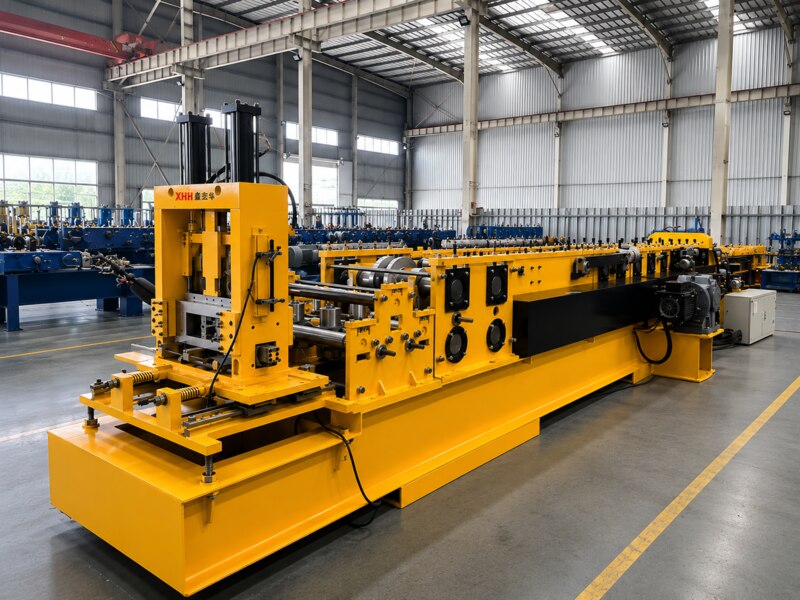
CZ100-300 Purlin Production Line with 23 Forming Stations
The CZ100-300 purlin production line combines 23 roll forming stations with PLC control, punching and cutting operations. It is designed for manufacturers producing C and Z steel purlins for engineered building systems.


The CZ100-300 purlin production line combines 23 roll forming stations with PLC control, punching and cutting operations. It is designed for manufacturers producing C and Z steel purlins for engineered building systems.
A purlin production line should be specified around the complete section drawing, material grade and connection pattern. This line integrates coil feeding and leveling, punching, forming and cutting so that the production sequence can be planned around the required members.
| Model / profile range | CZ100–300 |
|---|---|
| Machine dimensions | 11,000 × 1,800 × 1,500 mm |
| Main motor power | 5.5 kW × 2 |
| Hydraulic power | 11 kW |
| Forming stations | 23 |
| Listed forming speed | 30 m/min |
| Power supply | 380 V / 50 Hz / 3 phase |
| Roller material | GCr15 / Cr12; CNC machined, heat treated and hard-chrome plated |
| Cutter material | Cr12MoV |
| Control system | PLC |
The listed forming speed is a machine specification. Finished production output depends on member length, punching frequency, material and the selected operating sequence. Coil thickness, steel grade, flange and lip dimensions, and hole tooling are confirmed in the order specification.
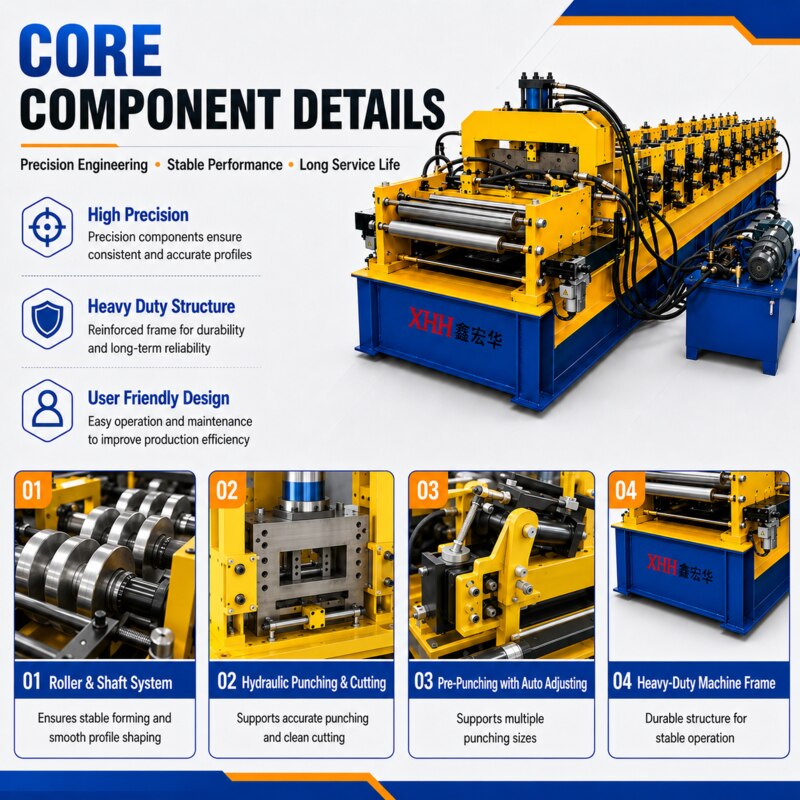
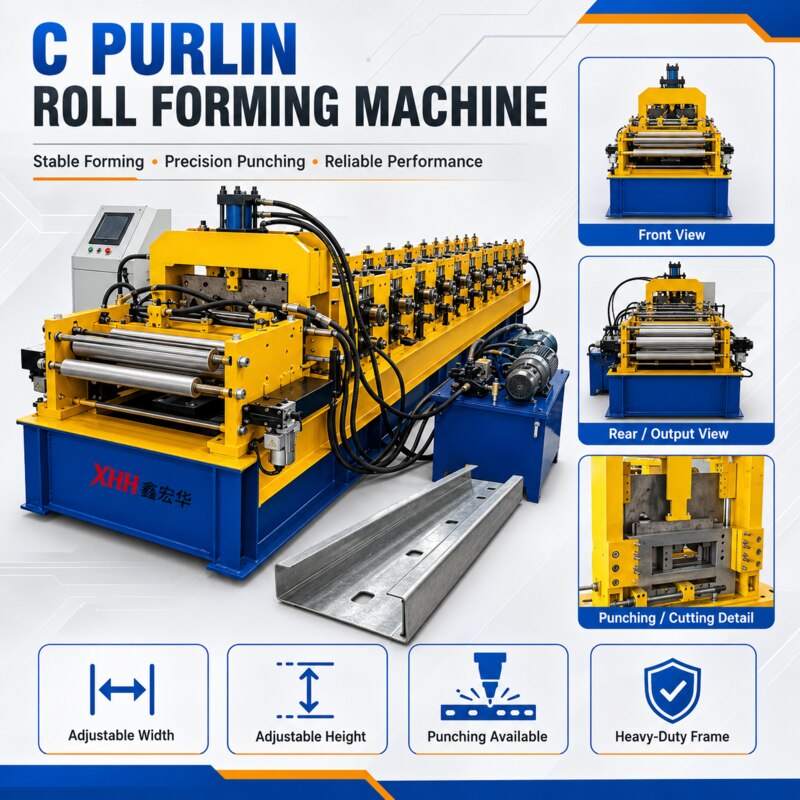
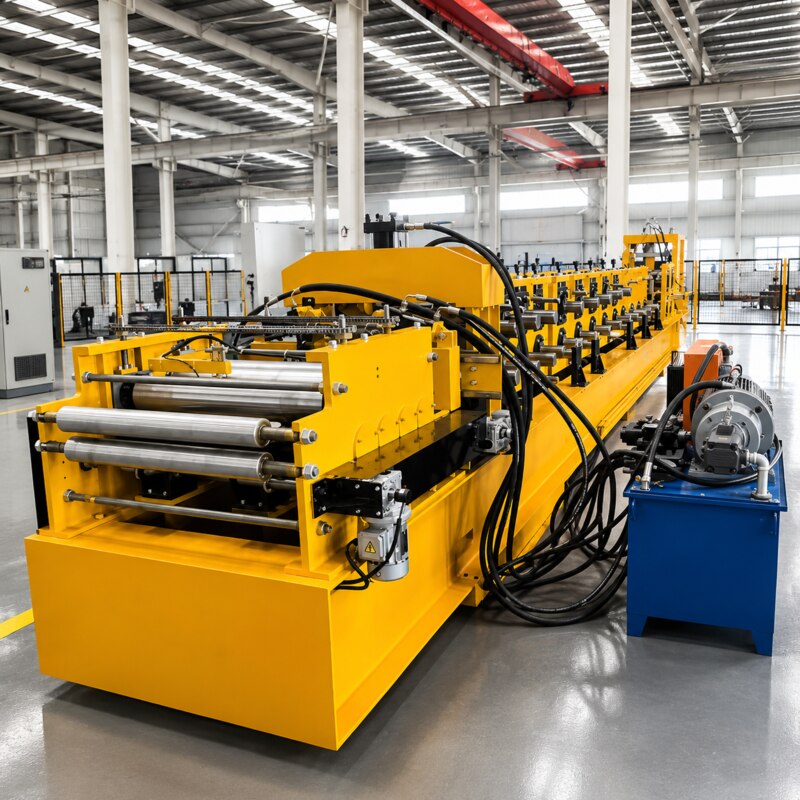
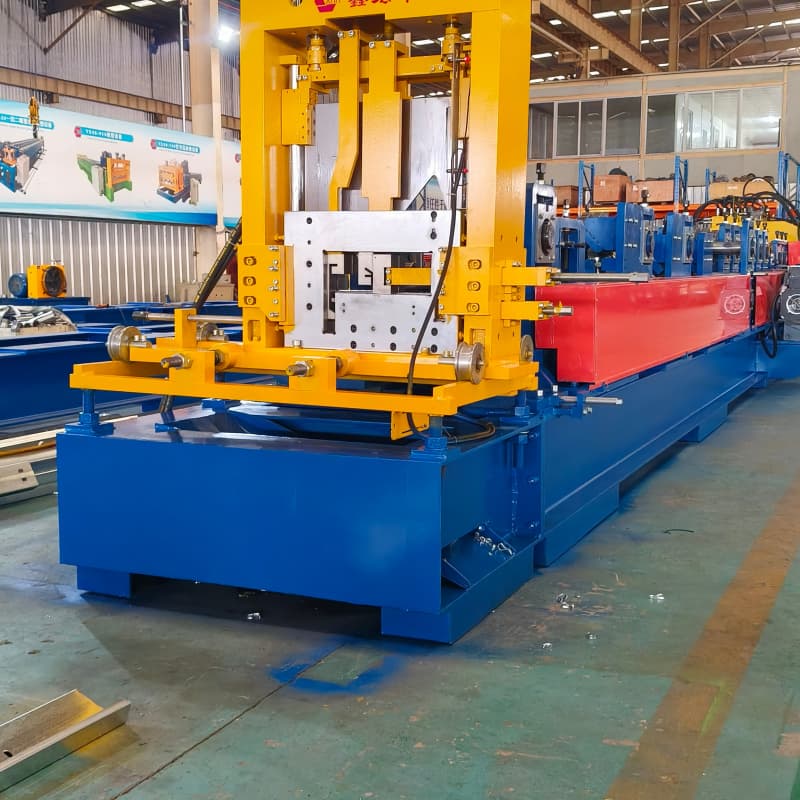
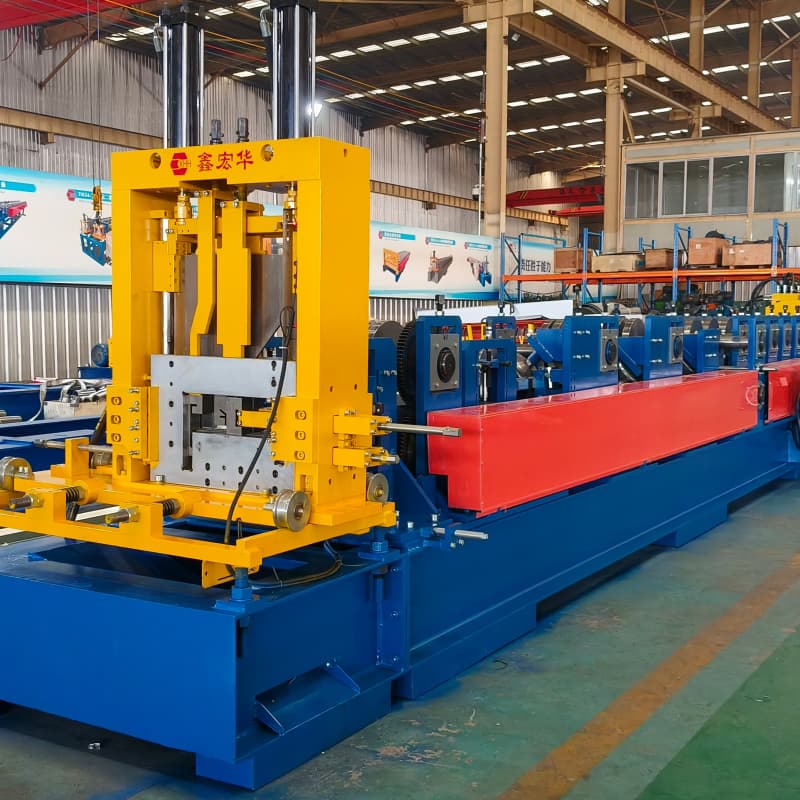
The forming system includes coil loading, leveling, punching, a forming section, cutting equipment, a hydraulic station and a control system. The final equipment arrangement is reviewed against the ordered profiles. The C-profile illustrations show the production application; the specification table defines this listed CZ100–300 configuration.
Inspect the first profiles for section geometry, straightness, cut length, hole position and end condition. Agree the sample drawings and acceptance criteria before testing. Representative short and long members help the buyer evaluate the planned product range.
Steel purlins are used as secondary members in engineered roof and wall cladding systems, including warehouses, industrial workshops and agricultural buildings. Section selection, spacing, connections and restraint requirements should follow the project design.
Can this machine produce both C and Z purlins?
The existing CZ100–300 configuration covers C and Z profile production. The exact section drawings and changeover procedure are confirmed for the ordered equipment.
What information is needed for a quotation?
Send the profile drawing, steel grade, thickness, coil width, member lengths, hole patterns and available power supply.
Can punching and cutting be configured for our products?
The tooling and operating sequence are discussed around your section and connection drawings. Confirm the included functions in the quotation.
Contact Xiamen Xinhonghua Machinery with your drawings and production requirements to discuss a C/Z purlin roll forming machine. Include the planned size range and material specification so that the forming, punching and cutting arrangement can be reviewed.
Related guide: Purlin profile dimensions and punching control.
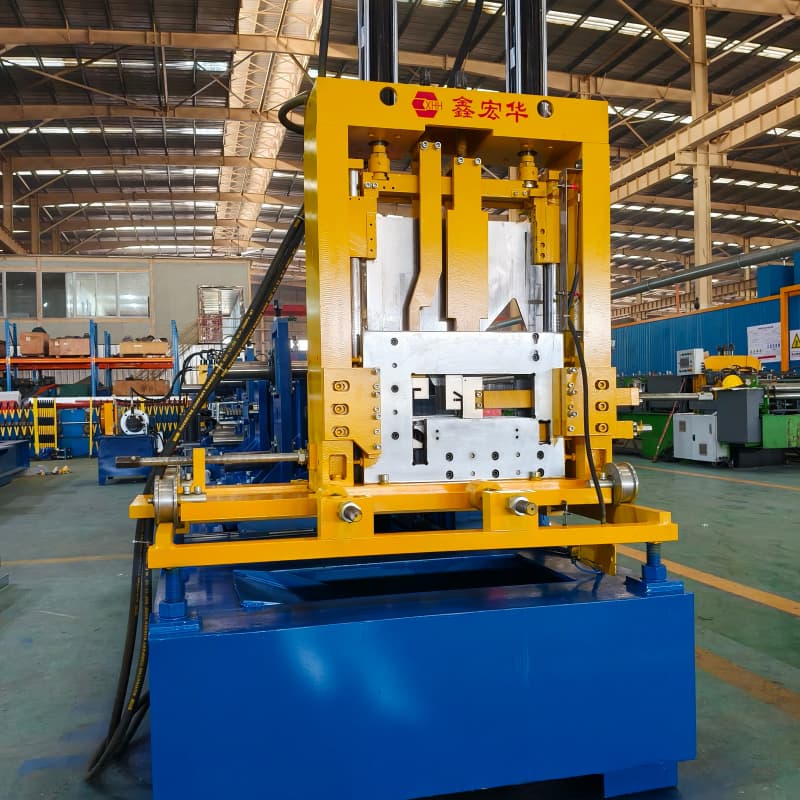
Switching between c and z purlins is seamless and saves a lot of production time.Computer control, fully automatic 1-minute changeover, no need for manual changeover.
Read More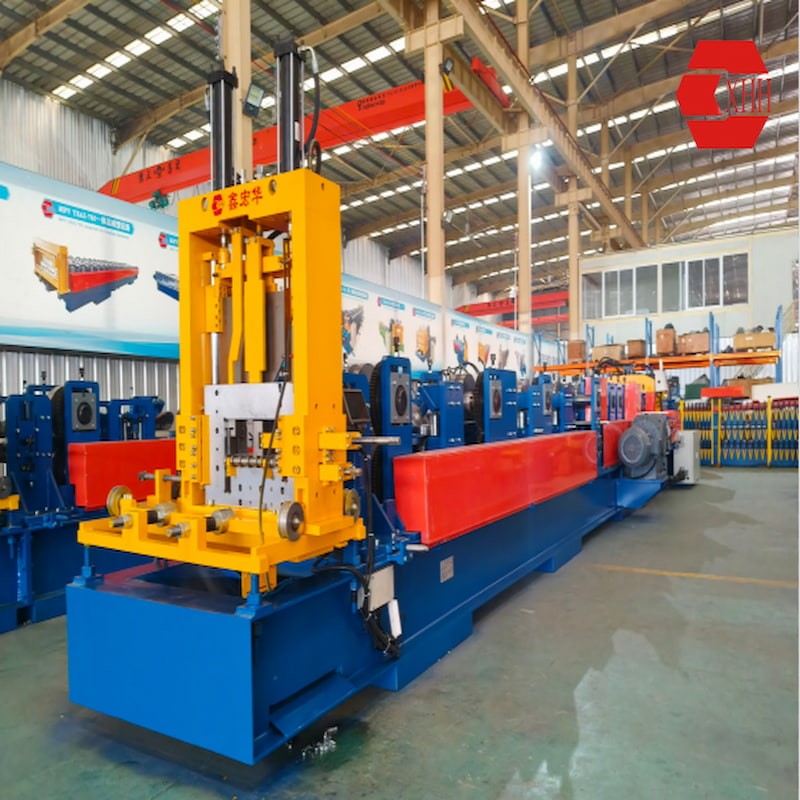
Switching between c and z purlins is seamless and saves a lot of production time.Computer control, fully automatic 1-minute changeover, no need for manual changeover.
Read More
It is a type of light keel steel forming machine primarily utilized for the production of studs and tracks in house framing. Its areas of application are particularly extensive, including factory decoration and warehouse cages. The roofs and new walls of locomotive hangars are constructed from the relevant products employed to press tiles.
Read More
Fully automatic C/Z integrated forming machine Automatically switches C-shaped steel width 100-300mm, waist height 30-100mm, Automatically switches Z-shaped steel width 120-300mm, waist height 30-100mm.
Read More
A automatically adjustment C/Z Channel Roll Forming Machine, C-shaped or Z-shaped metal channels.
Read More
It is a category of industrial machinery utilized in the construction and manufacturing sectors for the production of Z purlins. Full automatically change size from 120mm to 300mm by PLC control in 1 minute.
Read More
Make different purlin size without changing rollers or spacers. Quick change any size from 60mm to 250mm in 1min. Pre Cutting system(also can add post-cutter),no need changing cutter for different size. Easy to operate, low maintenance cost. Infinite sizing from 60-250mm,help to save material. Optional Punch hole at any position of purlin web and flange.
Read More
Create U-shaped channels or profiles from metal coils or sheets. Molding a continuous strip of metal by guiding it through a sequence of rollers to progressively achieve the intended profile.
Read More IPv6 network supported.
 +86 13605085003
 sunnie@xhhjx.com