Nov 05, 2026
Planning a C/Z purlin roll forming machine installation starts with the movement of material through the workshop. The machine footprint is only one part of the space required. Coil storage, loading access, finished-profile support, inspection and bundle removal all need to fit into a practical production route.
Start with the longest profiles you expect to make
List the normal product lengths and the longest profiles in the planned order mix. Use these lengths when discussing the discharge and runout arrangement with the equipment supplier. A layout that works for short samples may become congested when full-length roof purlins are produced. Check how finished members will be supported and removed without obstructing the next piece.
Draw the complete coil-to-bundle route
Mark receiving, coil storage, the decoiler, the forming line, inspection and finished-bundle storage on one drawing. Include columns, doors, existing equipment and the actual lifting or transport routes. Follow a representative coil and finished bundle through the proposed layout. Any repeated crossing or reversing movement is worth reviewing before the machine position is finalized.
Give loading and maintenance their own space
Confirm the loading method and the dimensions and weight of the coils to be used. Ask for the supplier's installation drawing and access requirements, including electrical cabinets, hydraulic equipment and service points. Keep the loading area and maintenance access available during ordinary production, rather than assuming stored bundles can always be moved when access is needed. Final clearances should follow the equipment documentation and the site's safety assessment.
Plan inspection before bundling
Provide a defined location to check profile dimensions, hole positions and cut length against the approved drawing. Keep accepted material separate from pieces awaiting a decision. If mixed C and Z orders are common, prepare clearly identified bundle positions for each profile, material and job. This reduces the chance that similar-looking members are packed together during a busy shift.
Connect layout decisions to the order mix
A line making long repeated batches may need a different storage arrangement from one switching frequently between small orders. Estimate how much work can accumulate at the discharge end while inspection, packing or transport takes place. Discuss the whole process with the supplier instead of comparing nominal forming speed alone. The aim is a flow that the people and handling equipment can sustain.
For scheduling different sizes, read our guide to mixed-size purlin production batches. For the checks carried out before packing, see profile dimension and punching control.
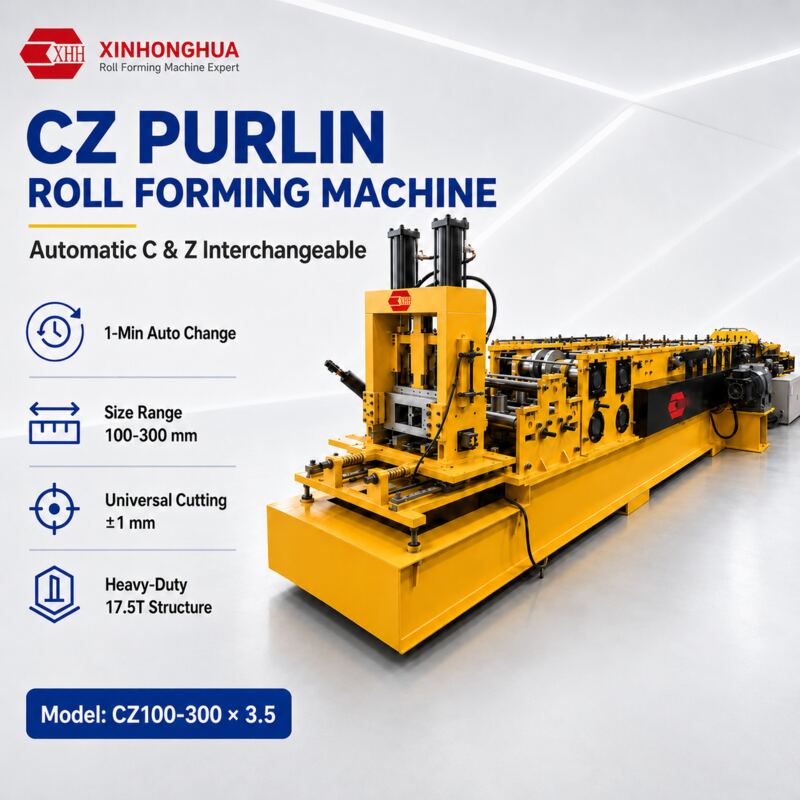
When preparing a C/Z purlin line enquiry for Xinhonghua, include a workshop sketch, intended product lengths, coil details and the available handling equipment. These inputs help turn a machine quotation into a workable installation discussion.
Read More

 IPv6 network supported.
 +86 13605085003
 sunnie@xhhjx.com


