Oct 13, 2026
A C/Z purlin roll forming machine should produce profiles that match the building drawings consistently. For a steel purlin manufacturer, the key checks are section geometry, straightness, cut length and punching position. Machine speed is useful only when finished members can be assembled without unnecessary rework.
Define the complete C and Z purlin drawings
A web-depth range alone does not describe a purlin. The production specification should include flange widths, lip dimensions, material thickness, steel grade, bend details and hole patterns. C purlins and Z purlins may require different tooling arrangements, and the available configurations must be confirmed for the quoted machine.
Provide the smallest and largest sections you plan to manufacture, together with the most frequently ordered intermediate sizes. This gives the supplier a clearer basis for evaluating the forming range and changeover process.
Control the incoming strip and entry alignment
Variation in material thickness, strength or strip width can affect the finished cross-section. Check coil documentation and keep material batches identifiable. The entry guide and feeding arrangement should keep the strip aligned with the forming line.
If a profile begins to twist or develop inconsistent flange dimensions, investigate both material and setup. Changing several settings at once makes the cause harder to identify. Follow the machine supplier's adjustment instructions and inspect new samples after each relevant change.
Measure the profile after forming
Inspect web depth, flange width and lip dimensions against the agreed drawing. Also check straightness and twist along the member. A profile that appears correct at one end may still be difficult to fit across its full length.
Set an inspection routine for the first pieces after a size change, a material change or a tooling adjustment. Use suitable measuring equipment and record the results. Acceptance tolerances should be agreed for the actual product and project rather than copied from a general machine advertisement.
Check punching against the connection details
A purlin punching machine configuration must match the required hole diameter, spacing and location. Check the distance from the member end to the first hole as well as the spacing between holes. Review whether the selected tooling can make the complete pattern shown in the drawing.
Connection fit-up is a useful practical check. Compare representative punched members with the specified cleats or connection templates. Structural hole requirements should come from the approved design; production convenience is not a reason to relocate them.
Verify cut length and the finished ends
Measure the cut length and inspect the end condition. Cutting sequence, material feeding and the selected tooling arrangement all form part of the production process. When comparing pre-cut and post-cut configurations, consider the required section range, material and punching sequence together.
Trial pieces should include both short and long members. A useful acceptance test also covers repeated production rather than a single successful sample. The objective is to confirm that the C/Z purlin machine can maintain the agreed quality throughout the defined test.
Make size changes repeatable
Record approved settings and establish a clear changeover procedure. Whether a particular machine uses manual adjustment, powered adjustment or an automatic size-changing arrangement must be confirmed in its specification. Automatic adjustment does not eliminate the need to inspect the first pieces.
Training should cover routine checks, safe setup and the correct response to out-of-tolerance profiles. Keeping the tooling clean and maintaining the equipment according to the supplier's instructions supports a stable production process.
What to include in a purlin machine inquiry
C and Z section drawings with the complete size range.
Steel grade, coating, thickness and coil width.
Hole drawings and the required cutting arrangement.
Typical member lengths and planned production quantities.
Agreed sample inspection and acceptance requirements.
Plan a production trial with Xinhonghua
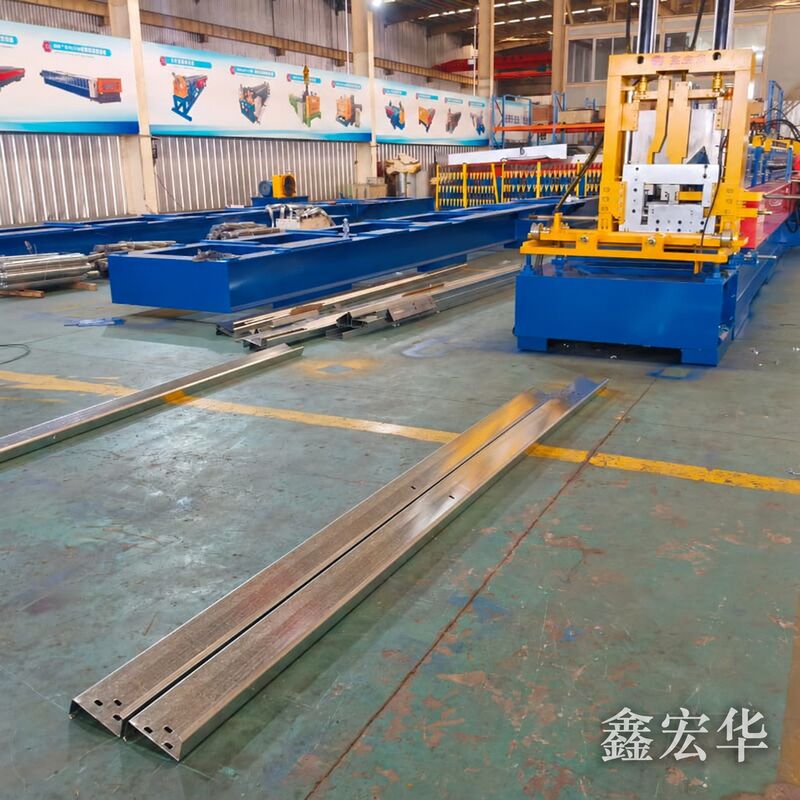
Xiamen Xinhonghua Machinery supplies roll forming equipment for steel profile production. For a C/Z purlin roll forming machine inquiry, send your section drawings and material requirements so that tooling, punching and size-change options can be discussed around the intended products.
Related reading: Pre-cut vs post-cut C/Z purlin machines.
Read More

 IPv6 network supported.
 +86 13605085003
 sunnie@xhhjx.com


